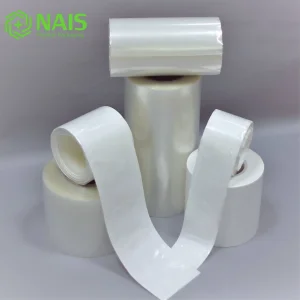
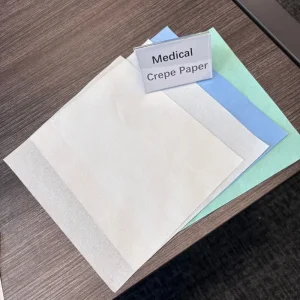
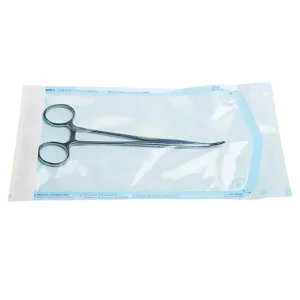
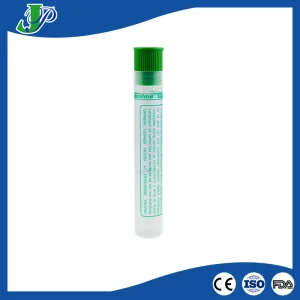
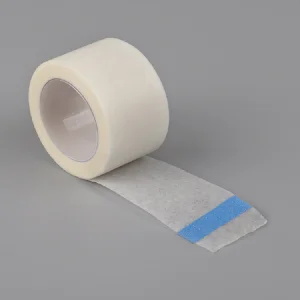
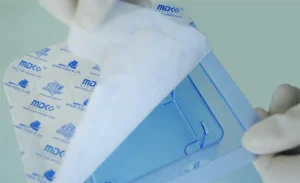
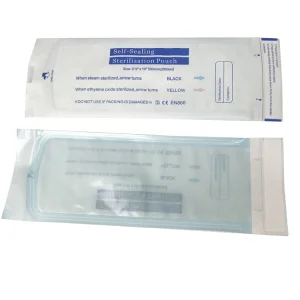
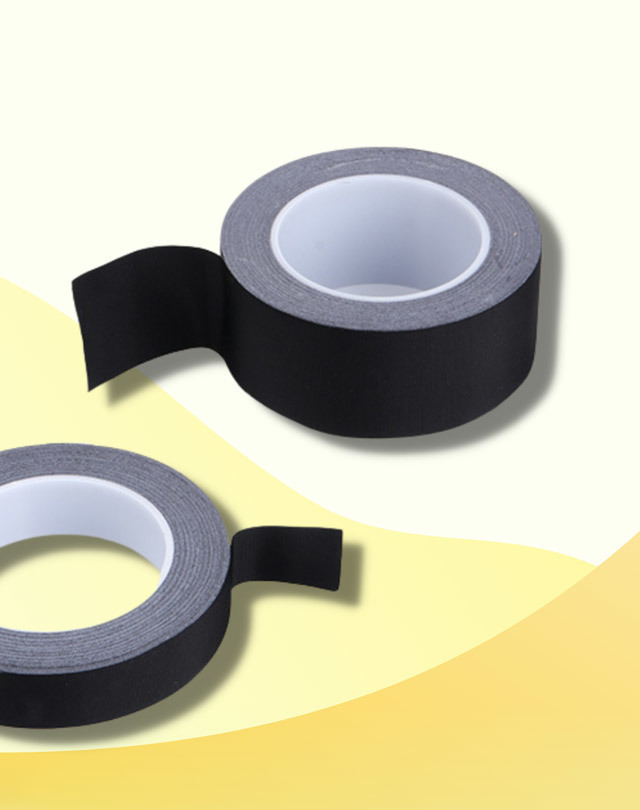
Guangzhou Jalil Medical Co., Ltd. is a leading manufacturer and supplier specializing in medical sterilization packaging and tape for healthcare facilities worldwide. With years of experience in the infection control and medical packaging industry, we provide high-quality solutions that ensure the safety and sterility of medical instruments. Our product range includes sterile pouches, autoclave sterilization wraps, chemical indicator strips, and sterilization tapes, all designed to meet rigorous international standards.
Committed to quality and innovation, Jalil Medical operates modern ISO-certified production facilities, combining advanced machinery with strict quality control to deliver consistent, reliable products. We support OEM and ODM services, allowing healthcare providers and distributors to access customized solutions that meet specific operational and regulatory requirements.
Explore our premium selection of medical-grade packaging materials engineered for supreme microbial barrier protection.
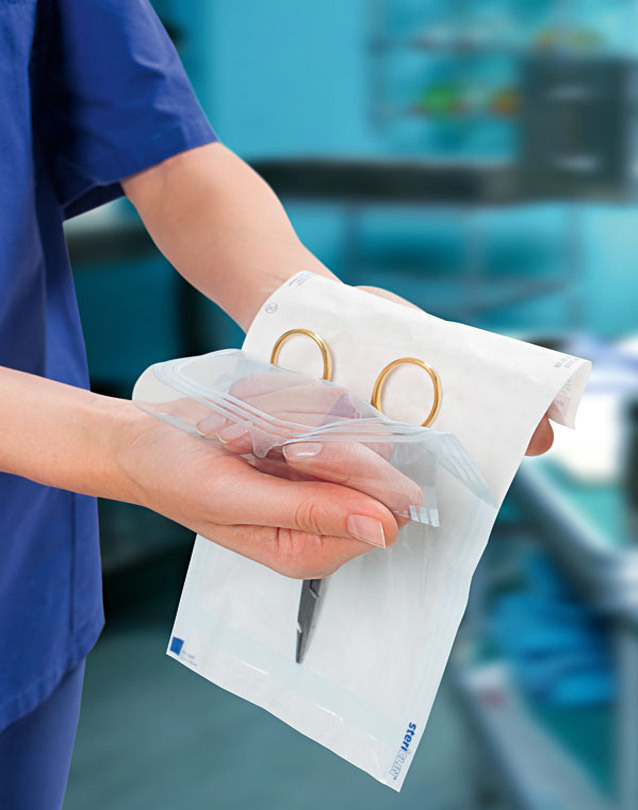
Our products are widely used in hospitals, clinics, laboratories, and surgical centers, helping healthcare professionals maintain infection-free environments. By integrating cutting-edge materials, color-changing indicators, and peelable packaging designs, we enhance usability and safety, ensuring instruments remain sterile until use.
As global healthcare standards tighten, the demand for high-integrity, heat-sealable sterilization bags continues to accelerate exponentially. Global procurement managers require supply chain resilience, strict traceability, and validated material performance.
International health systems demand zero-defect packaging rolls and pouches. Our products ensure compatibility with Steam, EO (Ethylene Oxide), and Gamma irradiation sterilization modalities, minimizing hospital-acquired infection (HAI) risks worldwide.
Utilizing high-density medical dialysis paper and multilayer PET/CPP transparent films, our heat-sealable lines deliver clean peel characteristics, high bursting strength, and airtight micro-pore filtration barriers.
We are investing heavily in eco-friendly biodegradable medical papers, smart RFID-tracked sterilization batches, and automated indicator monitoring systems to shape the next decade of sustainable infection control.
Discover our comprehensive inventory tailored for surgical suites, dental clinics, and specialized pharmaceutical lab requirements.
At Guangzhou Jalil Medical, our mission is to provide trusted, cost-effective, and environmentally responsible sterilization packaging solutions. We pride ourselves on excellent customer service, timely delivery, and continuous innovation to meet the evolving needs of the healthcare industry.
Whether for small clinics or large hospitals, Jalil Medical is a reliable partner for high-quality medical sterilization packaging and tape.
Find expert insights and technical clarifications regarding our heat-sealable sterilization bags and global export services.
Our sterilization pouches and rolls are fully compatible with Steam (Autoclave), Ethylene Oxide (EO), and Gamma irradiation sterilization processes, featuring distinct color-changing chemical indicator inks for immediate visual verification.
Yes, we provide comprehensive OEM and ODM services, including customized dimensions, printing with your corporate brand logo, tailored packaging configurations, and specific regulatory documentation support.
Our production facilities operate under stringent ISO-certified quality management systems, and our medical packaging products adhere to CE and international regulatory compliance requirements for clinical safety.
We utilize moisture-resistant, heavy-duty corrugated export cartons and palletized shrink-wrapping to protect all sterile reels, pouches, and indicator tapes against environmental damage during transit across global supply chains.
 Jalil Medical