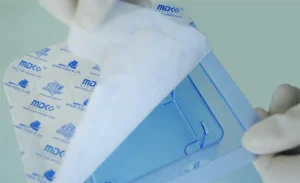
Precision-engineered medical wraps and laminates tested for high humidity resistance and extended microbial shelf-life.
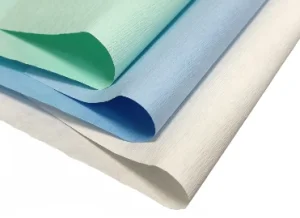
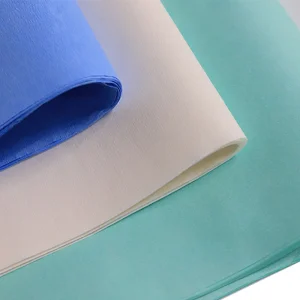
Guangzhou Jalil Medical Co., Ltd. is a leading manufacturer and supplier specializing in medical sterilization packaging and tape for healthcare facilities worldwide. With years of experience in the infection control and medical packaging industry, we provide high-quality solutions that ensure the safety and sterility of medical instruments. Our product range includes sterile pouches, autoclave sterilization wraps, chemical indicator strips, and sterilization tapes, all designed to meet rigorous international standards.
Committed to quality and innovation, Jalil Medical operates modern ISO-certified production facilities, combining advanced machinery with strict quality control to deliver consistent, reliable products. We support OEM and ODM services, allowing healthcare providers and distributors to access customized solutions that meet specific operational and regulatory requirements.
Global Quality Assurance: Certified under ISO 13485, ISO 11607, and CE standards to guarantee zero-defect barrier integrity during maritime transport and tropical storage.
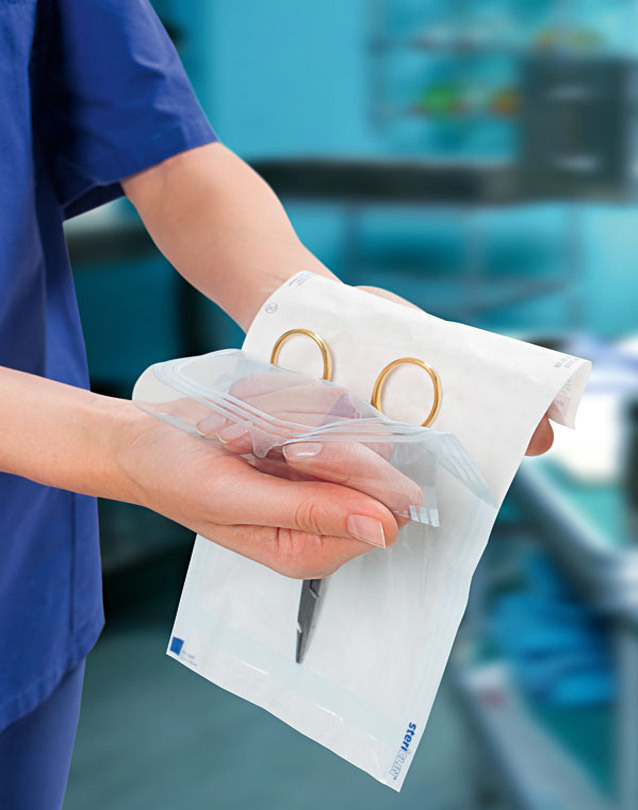
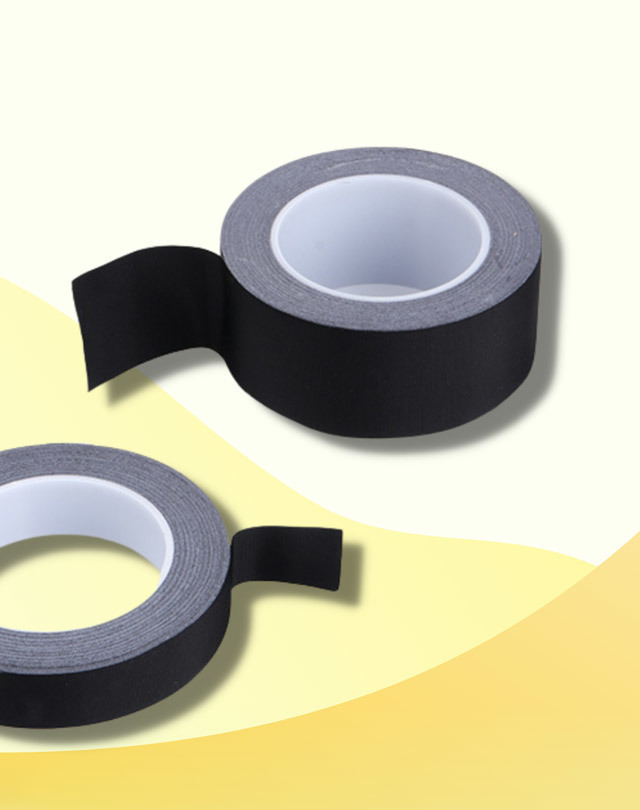
Our products are widely used in hospitals, clinics, laboratories, and surgical centers, helping healthcare professionals maintain infection-free environments. By integrating cutting-edge materials, color-changing indicators, and peelable packaging designs, we enhance usability and safety, ensuring instruments remain sterile until use.
At Guangzhou Jalil Medical, our mission is to provide trusted, cost-effective, and environmentally responsible sterilization packaging solutions. We pride ourselves on excellent customer service, timely delivery, and continuous innovation to meet the evolving needs of the healthcare industry. Whether for small clinics or large hospitals, Jalil Medical is a reliable partner for high-quality medical sterilization packaging and tape.
Request Technical DatasheetsNoro, located in the Western Province of the Solomon Islands, occupies a strategically essential position as a major maritime hub, commercial port, and industrial center in the South Pacific. As the region experiences modernizations in local healthcare logistics, port-side medical centers, and fish processing plant quality control laboratories, the demand for high-integrity sterile barrier packaging has reached an all-time high.
Noro features a high-humidity tropical marine environment. Standard packaging paper frequently absorbs moisture, compromising seal strength and microbial barrier capabilities. Our specialized medical-grade virgin wood pulp paper and multi-layer film laminates are hydrophobic and heat-stable, preventing moisture ingress and mold growth during storage.
From the Helena Goldie Hospital infrastructure network to shipboard infirmaries operating out of Noro Port, sterilization workflows demand packaging that guarantees sterility despite transport vibrations, ocean fog exposure, and prolonged inventory turnover cycles.
Beyond human clinical care, Noro's thriving tuna processing and marine export industries require sterile sampling tool packaging, quality-assurance laboratory supplies, and environmental testing consumables sealed in high-burst-strength sterile barrier film reels.
Information Gain Insight: Unlike standard commercial paper wraps, medical-grade paper combined with PET/CPP multi-layer film laminates offers controlled porosity. This allows steam, ethylene oxide (EO), or formaldehyde gas sterilants to penetrate freely during processing, while establishing a impenetrable tortuous path against airborne pathogens once cooling and drying cycles complete.
The global sterile barrier system (SBS) sector is transitioning rapidly toward standardized high-performance composite laminates. Regulatory updates under ISO 11607 Parts 1 & 2 demand continuous validation of seal integrity, visual peelability without fiber shedding, and long-term aging stability.
| Parameter | Standard Crepe Wrapping Paper | Medical Grade Dialysis Paper | PET/CPP Laminated Film Reels |
|---|---|---|---|
| Material Base | 100% Virgin Wood Pulp Crepe (60g/m²) | Reinforced Fiber Synthetic Paper (60g - 70g) | Multi-Layer Co-extruded Polyester/Polypropylene |
| Sterilization Compatibility | Autoclave Steam, EO Gas, Gamma | Autoclave Steam, EO Gas, Formaldehyde | Steam Autoclave (121°C - 134°C), EO Gas |
| Microbial Barrier (LRV) | > 98.5% Efficiency | > 99.9% Efficiency | 100% Hermetic Impermeable Barrier |
| Peel Characteristics | Wrapping / Folding Technique | Peelable with minimal linting | Fiber-free clean peel along seal seams |
| Indicator Integration | External indicator tape required | Dual Water-based Process Indicators | Tinted film view + Process Indicators |
| Shelf-Life (Noro Humidity) | Up to 6 Months (Double Wrapped) | Up to 12 Months | Up to 5 Years (Under Seal Integrity) |
Guangzhou Jalil Medical Co., Ltd. leverages China’s unmatched advanced chemical manufacturing ecosystem and automated high-speed lamination technology. By integrating raw material sourcing, multi-color process indicator printing, precision slitting, and cleanroom pouch converting into a unified workflow, we deliver exceptional price-performance metrics without compromising quality.
Hospitals and health authority procurement officers in Noro and Western Province can directly access complete compliance dossiers, including:
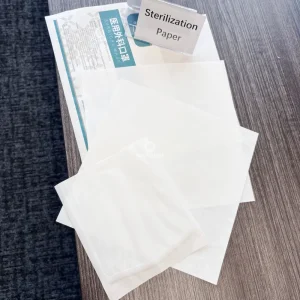
Explore our complete inventory of medical crepe papers, dialysis rolls, and Tyvek sterile barrier laminates.
Every clinical and industrial operational setting demands customized sterile packaging formats tailored to equipment geometries and exposure vectors. Guangzhou Jalil Medical provides modular options designed for immediate integration into diverse regional setups:
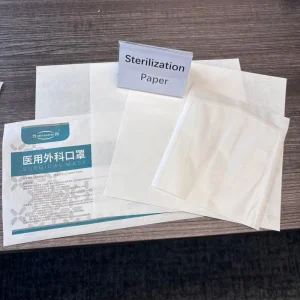
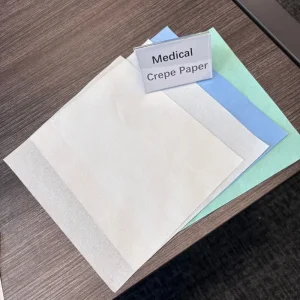
Designed for double-wrapping heavy surgical trays, orthopedic toolsets, and general surgical packs. The high drapability of our 60g crepe paper prevents memory back-spring when opened sterilely in operating rooms across Noro healthcare centers.
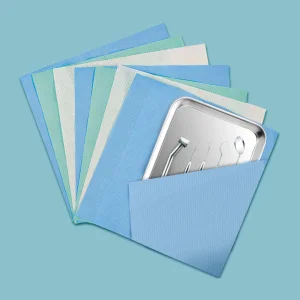
Pre-formed peel pouches and custom-width dialysis paper reels enable rapid sealing of handpieces, scalers, and mirrors. Transparent multi-layer film allows instant visual identification of dental instruments without opening the sterile barrier.
Solomon Islands maritime food export laboratories require reliable sampling swab wrap, petri dish wrapping, and sterile barrier pouches for quality testing instruments, preventing cross-contamination during transit.
Essential technical clarifications for healthcare procurement directors, CSSD managers, and medical importers in Noro.
Partner with Guangzhou Jalil Medical Co., Ltd. for certified quality, highly competitive factory-direct pricing, and dependable global shipping to the Solomon Islands.
 Jalil Medical